 EN


What Is PCHR? A Boiler Condensate Recovery Solution That Can Reduce Fuel Consumption by Up to 20%
In many industrial steam plants, seeing steam rising from a feedwater tank or deaerator tank is often considered a normal part of boiler operation.
However, generating that steam requires a significant amount of fuel.
What many facilities overlook is that much of this lost thermal energy can actually be recovered and reused.
One solution is the PCHR system, a condensate recovery technology designed to maintain the original pressure and temperature of condensate before returning it to the boiler. By preserving this remaining energy, PCHR can significantly reduce steam production costs.
Table Of Contents
Quick Summary
- Industrial steam is commonly used in two ways: direct steam applications and indirect heat transfer applications.
- In indirect applications, steam condenses into condensate after transferring its heat.
- Condensate still contains a substantial amount of usable thermal energy.
- When hot condensate is discharged into an atmospheric tank, part of it flashes into steam and escapes to the environment.
- PCHR preserves condensate pressure and temperature before returning it to the boiler.
- In the case presented, fuel consumption was reduced from approximately 200 kg of rice husk to 165 kg per ton of steam produced.
- The fuel-saving potential reached approximately 20%.
I. How Is Steam Used In Industrial Facilities?
In industrial steam systems, steam is generated by a boiler and distributed to process equipment throughout the production line.
The purpose of steam is to transfer thermal energy from the boiler to various manufacturing processes.
Typical applications include:
- Product drying
- Sterilization
- Laundry and garment pressing
- Food steaming and cooking
- Process heating applications
In practice, steam is generally used through two different methods.
 Industrial boilers supply steam for a wide range of manufacturing and process heating applications.
1. Direct Steam Applications
Direct steam applications involve injecting steam directly into the product being processed.
Examples include:
- Steamed buns
- Rice paper production
- Rice steaming
- Various food steaming processes
In these applications, steam comes into direct contact with the product and becomes part of the production process.
2. Indirect Steam Applications
In indirect steam applications, steam does not come into direct contact with the product.
Instead, thermal energy is transferred through a heat exchanger to support the manufacturing process.
After releasing its heat, the steam condenses into condensate.
This condensate is typically collected and returned to the boiler system as feedwater.
This is also where the energy-saving opportunity discussed in this article begins.
Learn more: What Is a Steam Boiler? Structure, Working Principle, and Industrial Applications
II. Why Does Condensate Still Contain Significant Thermal Energy?
Many people assume that once steam has transferred its heat and condensed into water, most of its energy has already been consumed.
In reality, condensate leaving the heat transfer process still contains a substantial amount of thermal energy.
Steam typically enters process equipment at approximately 8 bar pressure.
After heat transfer and system pressure losses, the remaining condensate may still be at around 4 bar.
At this pressure, condensate temperature remains approximately 144°C.
This means that even though the steam has condensed back into water, it still carries a considerable amount of usable heat energy.
If this heat is allowed to escape into the environment, additional fuel will be required to reproduce the same amount of energy inside the boiler.
Why Is 144°C Such An Important Temperature?
When condensate at approximately 144°C is discharged into an atmospheric tank, its thermodynamic equilibrium changes immediately.
As a result, a portion of the condensate flashes into steam and escapes into the surrounding environment.
This is the reason why steam is often seen rising from feedwater tanks and deaerator tanks in many industrial facilities.
At first glance, this may appear to be a normal operating condition.
However, that visible steam represents thermal energy that was originally generated by burning fuel and is now being lost to the atmosphere.
Learn More: The Benefits of a Deaerator Tank in Boiler Systems
III. Why Heat Is Lost In Conventional Condensate Recovery Systems
In conventional condensate recovery systems, hot condensate is typically returned to a feedwater tank or deaerator operating at atmospheric pressure.
When high-temperature condensate enters a lower-pressure environment, part of its energy is released as flash steam.
This creates the visible steam plume commonly observed around feedwater tanks in many boiler plants.
It is important to understand that this steam is not generated for free.
The thermal energy contained in that steam was originally produced by consuming fuel in the boiler.
Therefore, steam escaping from a feedwater tank is not merely an operational phenomenon - it is a direct source of increased steam production costs.
 Steam released from a condensate storage tank due to heat loss
IV. A Real-World Example Of Heat Loss From Condensate
The amount of thermal energy remaining in condensate is often far greater than many people realize.
Consider the following example.
To cool 1 cubic meter of condensate at approximately 144°C to below 100°C without flash evaporation, nearly 10 cubic meters of cold water would be required.
For a 10-ton-per-hour steam boiler with a condensate return rate of approximately 40%, the returned hot condensate volume would be around 4 cubic meters per hour.
Cooling this entire volume would require approximately 40 cubic meters of cold water every hour.
In reality, the boiler makeup water flow is typically only around 6 cubic meters per hour.
This significant difference demonstrates that there is not enough cold water available to cool all returned condensate below 100°C.
As a result, a substantial amount of thermal energy escapes as flash steam.
V. What Is The PCHR Solution?
Once the source of heat loss in the condensate recovery process has been identified, the next question is how to retain that energy within the system.
PCHR is a solution designed to minimize heat losses during condensate recovery before the condensate is returned to the boiler.
The primary objective of the system is to recover and reuse the remaining thermal energy contained in the condensate rather than allowing it to be lost to the surrounding environment during operation.
VI. How Does PCHR Work?
After the heat transfer process, the condensate still remains at approximately 4 bar pressure and 144°C.
Instead of discharging this hot condensate into an atmospheric tank where flash evaporation can occur, the proposed solution is to maintain its original pressure and temperature.
The condensate is then returned directly to the boiler.
By preserving the condensate at approximately 4 bar and 144°C and pumping it directly back into the boiler system, heat losses caused by flash steam can be eliminated.
As a result, thermal energy that would otherwise be lost is retained and reused within the steam generation system.
The primary objective of the system is to recover and reuse the remaining thermal energy contained in the condensate rather than allowing it to be lost to the surrounding environment during operation.
 PCHR Solution Maximizes Heat Recovery from Condensate
VII. Technical Challenges In Condensate Recovery
To successfully implement this solution, two major engineering challenges must be addressed.
First Challenge: Maintaining Condensate Pressure
The first challenge is maintaining condensate pressure at approximately 4 bar, or at the desired operating pressure.
At the same time, this pressure retention must not interfere with the plant's production process.
This is essential to preserve the remaining thermal energy contained in the condensate before it is returned to the boiler.
Second Challenge: Pumping High-Temperature Condensate Back To The Boiler
In addition to maintaining pressure, the system must also be capable of returning condensate at approximately 144°C back to the boiler.
This is one of the key technical requirements highlighted in the proposed solution.
When both challenges are addressed successfully, the remaining heat contained in the condensate can be recovered and reused instead of being lost to the environment.
VIII. Real-World PCHR Installation Project
The PCHR solution has been implemented in a variety of industrial facilities across different sectors.
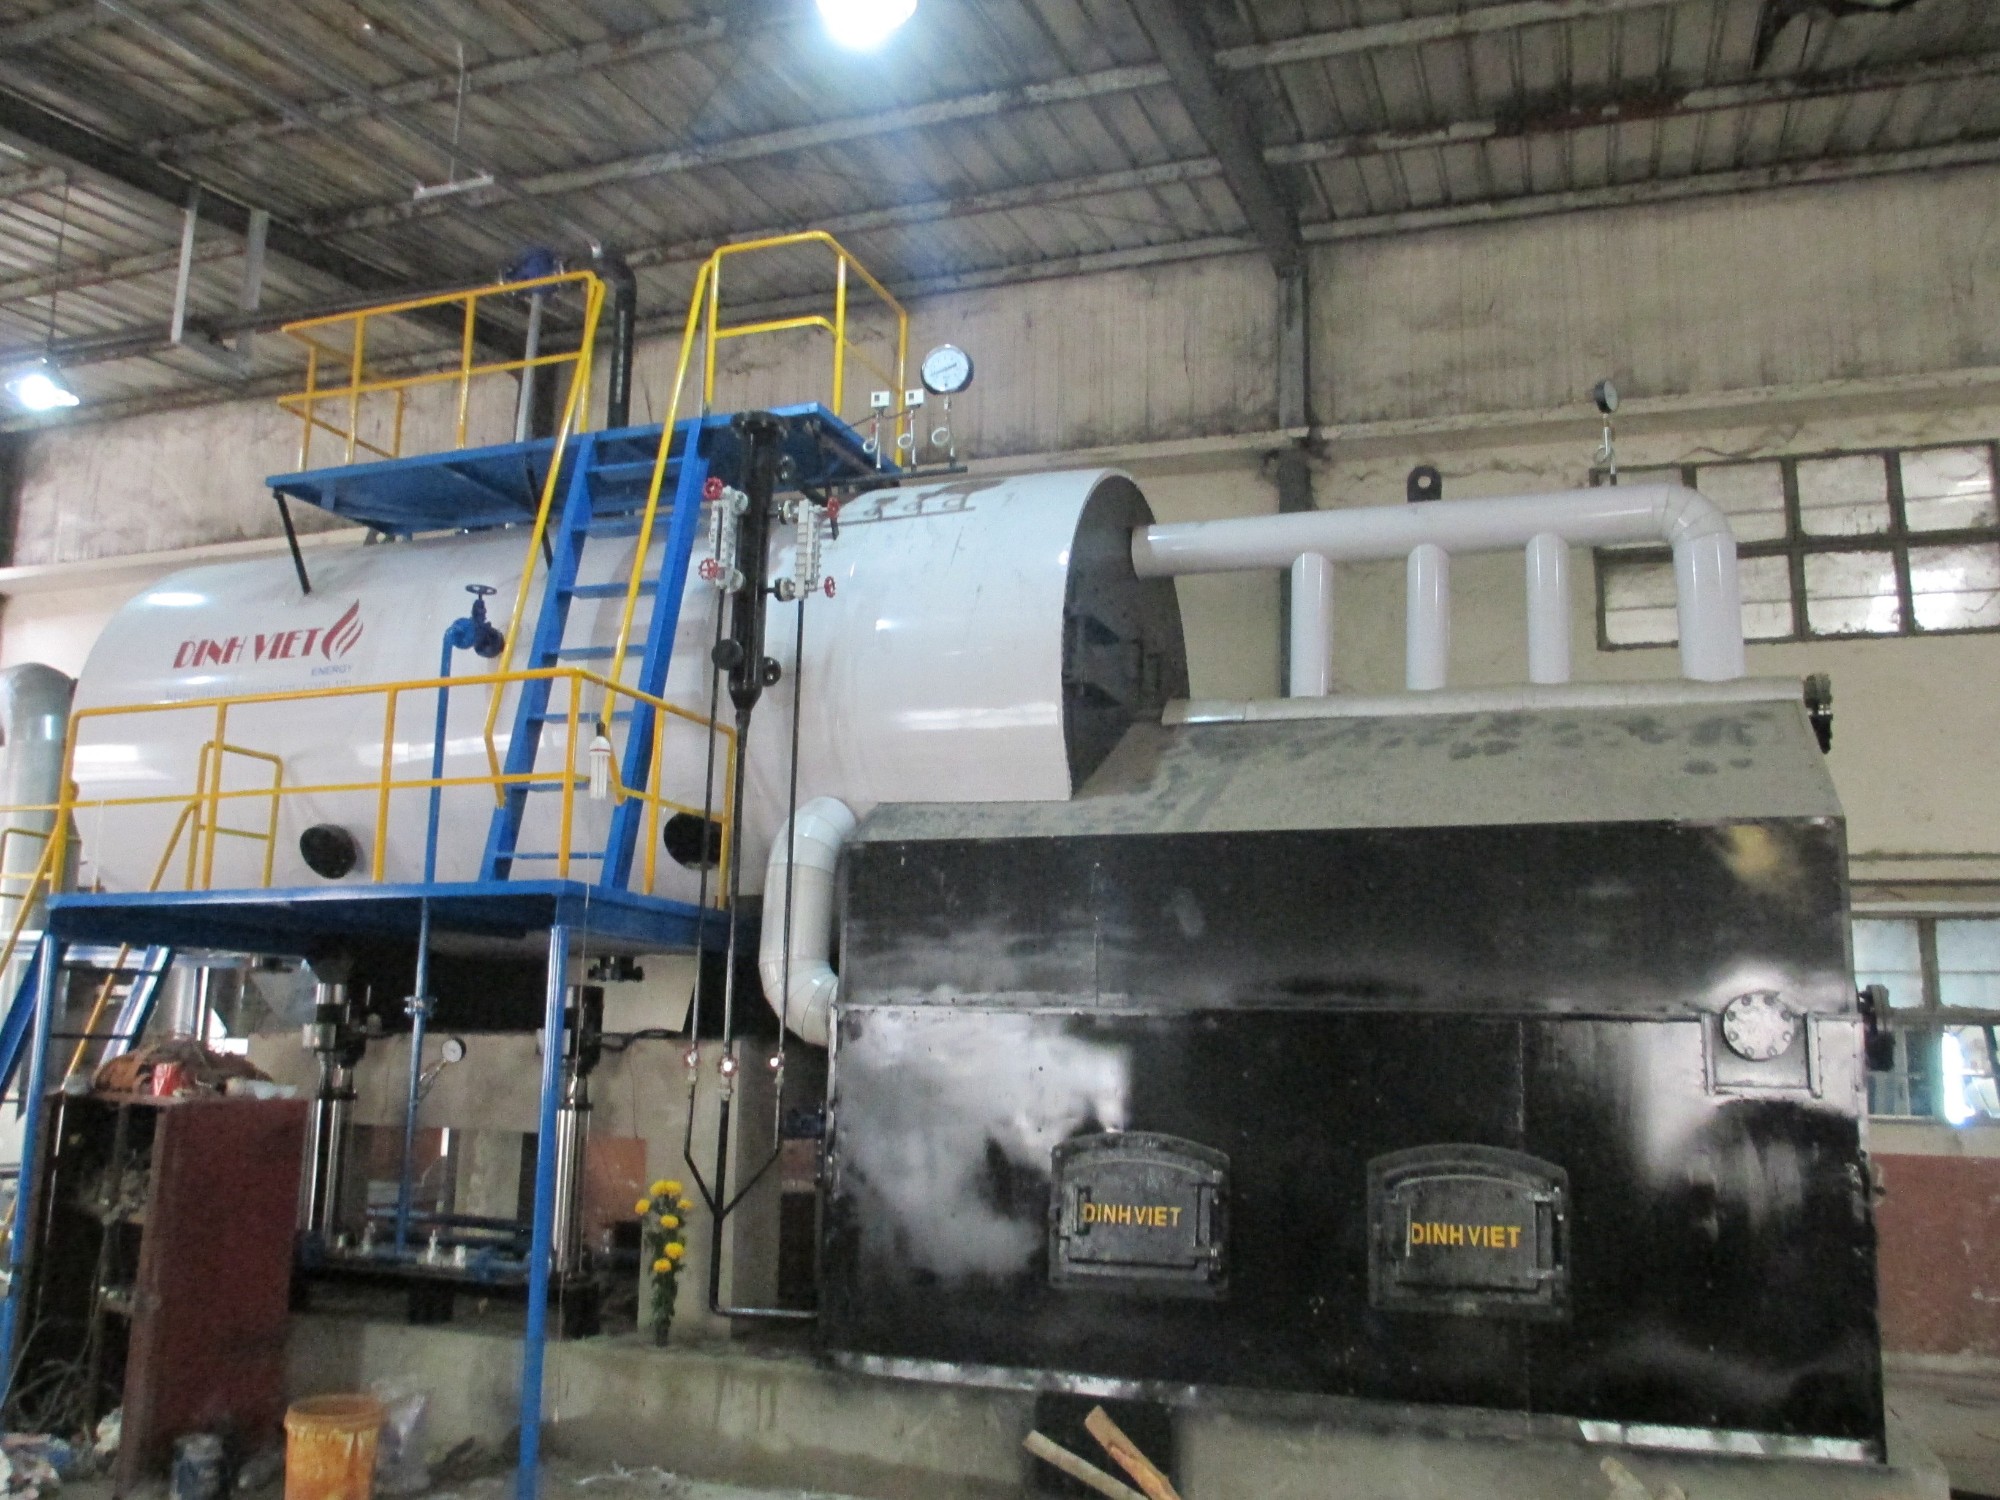
One of the projects referenced involves two 15-ton-per-hour fluidized bed boilers fired by rice husk at the CHISECO plant, a member of the Sao Mai Group in An Giang Province.
This project serves as a practical example for evaluating the effectiveness of high-pressure condensate recovery.
Following system commissioning, fuel consumption showed a significant improvement.
IX. Fuel-Saving Performance Of The PCHR System
Before implementing the PCHR system, fuel consumption was approximately 200 kg of rice husk per ton of steam produced.
After installation, fuel consumption decreased to approximately 165 kg of rice husk per ton of steam.
This represents a reduction of roughly 20% in steam production costs.
The project also reported that the 15-ton boiler system was able to operate comfortably at around 16 tons after the solution was implemented.
However, system performance depends heavily on the condensate return rate.
If condensate recovery is below 30%, the fuel-saving benefits may not be significant.
Conversely, when condensate recovery exceeds 30%, the reported payback period for continuously operating boilers is less than six months.
 Real-World Application of the PCHR Condensate Recovery System
X. When Should You Invest In A PCHR System?
Not every steam system will achieve the same level of benefit from condensate recovery.
The most important factor to evaluate is the condensate return rate.
When condensate recovery is low, fuel-saving results may be limited.
On the other hand, systems with higher condensate return rates can retain significantly more thermal energy within the process.
A condensate return rate of approximately 30% is referenced as a useful benchmark when evaluating the economic viability of the solution.
The discussion also focuses on continuously operating boiler systems where hot condensate is consistently returned during production.
XI. Key Takeaways About The PCHR System
- Condensate still contains a substantial amount of thermal energy after heat transfer
- Heat losses during condensate recovery can increase boiler fuel consumption.
- PCHR is designed to recover and reuse the remaining energy contained in condensate.
- System performance depends on operating conditions and condensate return rates.
- In the case study presented, the solution reduced fuel consumption and shortened the investment payback period.
These are the key factors to consider when evaluating condensate energy recovery opportunities in industrial steam systems.
XII. FAQ – Frequently Asked Questions
1. What Is PCHR?
PCHR is a condensate recovery solution designed to preserve the original pressure and temperature of condensate before it is returned to the boiler, minimizing heat loss within the steam system.
2. Why Does Condensate Still Have Value?
After transferring heat, steam condenses into water but still retains a substantial amount of thermal energy.
Condensate remains at approximately 144°C and 4 bar pressure after the heat exchange process.
3. Why Does Condensate Lose Heat?
When hot condensate is discharged into an atmospheric tank, part of the water flashes into steam and escapes into the surrounding environment.
This escaping steam represents thermal energy that is lost from the system.
4. What Fuel Savings Were Reported?
Fuel consumption was reduced from approximately 200 kg of rice husk per ton of steam to around 165 kg per ton of steam.
→ This represents a fuel-saving improvement of approximately 20%..
5. Which Steam Systems Are Suitable For PCHR?
The effectiveness of the solution depends largely on the condensate return rate.
When condensate recovery is low, fuel-saving benefits may be limited.
6. Why Do Many Factories Overlook This Energy Loss?
In many facilities, steam rising from feedwater tanks is considered a normal operating condition.
However, that visible steam is actually generated from the remaining heat stored in the condensate and represents energy that has already been produced using boiler fuel.
Is Your Steam System Losing Valuable Heat Through Condensate?
In many industrial facilities, steam rising from a feedwater tank or deaerator is often regarded as a normal operating condition.
However, this may indicate that valuable thermal energy is being lost to the atmosphere instead of being retained within the system.
If your facility already recovers condensate but frequently experiences this phenomenon, a system assessment may help identify hidden energy losses and evaluate opportunities for recovering the remaining heat contained in the condensate.
Technical Consultation Hotline: +84 942 488 818
XIII. Conclusion
In many industrial steam systems, a significant amount of thermal energy remains in condensate after heat has been transferred to the process.
When hot condensate is returned to an atmospheric tank, part of that energy is released and lost as flash steam.
The PCHR solution is designed to preserve condensate pressure and temperature before returning it to the boiler, thereby minimizing this heat loss.
By recovering and reusing the remaining energy in condensate, facilities can significantly reduce fuel consumption and improve overall steam generation efficiency.
Other news
-
Industrial Boiler Applications: 6 Common Uses and High-Temperature Heating Solutions
19/08/2026, -
Boiler Types by Design: Water-Tube, Fire-Tube, Single-Drum and Two-Drum Boilers
15/08/2026, -
Fluidized Bed Boiler: Design, Working Principle, Advantages and Disadvantages
07/08/2026, -
What Is a Boiler? How Boilers Work and the Main Types by Fuel
28/07/2026, -
8 ENERGY LOSS POINTS THAT INCREASE BOILER FUEL CONSUMPTION AND HOW TO FIX THEM
17/07/2026, -
3 Key Factors That Reduce Boiler Fuel Consumption
08/07/2026, -
Proper Boiler Blowdown Procedure | Safe Boiler Blowdown Valve Operation Guide
24/06/2026, -
What Is a Steam Separator? Real-World Testing of Steam Moisture Separation Performance
20/06/2026, -
CHAIN GRATE BOILER VS FLUIDIZED BED BOILER: WHICH TECHNOLOGY IS BETTER FOR YOUR FACTORY?
18/06/2026, -
Oil-Fired Steam Boiler For Chemical Tank Heating
15/06/2026,


DIVI GROUP CO., LTD
Office: 588 Pham Van Chieu street, ward 16, Go Vap district, Ho Chi Minh city, Viet Nam
Factory: Khanh Binh 10 street, Khanh Van quarter, Khanh Binh ward, Tan Uyen city, Binh Duong province, Viet Nam
Hotline: +84 942 488 818
Tel: 0274 3800 338
Email: info@divigroup.com.vn
Business license : 0311016524, issue date : 26/07/2011 by Department of Planning and Investment of Ho Chi Minh City
Representatives: Lê Văn Hiếu
Online :
Vistited :