 EN


What Is a Boiler? How Boilers Work and the Main Types by Fuel
Prepared by: DIVI Group Technical Team
Technical review: Engineer Lê Văn Hiếu – Founder and CEO of DIVI Group
In most industrial plants today, steam is an important source of energy used in processes such as heating, drying, steaming, sterilization, concentration, and power generation.
Although boilers are widely used across many industries, not every business clearly understands what a boiler is, how it works, or which boiler technology is most suitable for its operational requirements.
In this article, you will learn:
-
What is a boiler?
-
How does a boiler work?
-
How are industrial boilers classified?
-
What are the differences between fixed-grate and chain-grate boilers?
This is the first article in the “What Is a Boiler?” series. The next part will introduce other solid-fuel combustion technologies.
Table Of Contents
I. What Is a Boiler?
A boiler is an enclosed, heat-resistant and pressure-resistant piece of equipment that contains water.
It uses heat generated from fuel combustion to heat the water, bring it to boiling point, and convert it into steam.
Once generated, the steam is transported through a piping system to equipment throughout the plant, where it is used in various production processes, including:
-
Steaming
-
Drying
-
Heating
-
Concentration
-
Sterilization
-
Distillation
-
Hot pressing
-
Power generation
Steam may serve different purposes depending on the industry. However, the fundamental operating principle of a boiler remains the same.
II. How Does a Boiler Work?
In simple terms, a boiler converts the energy stored in fuel into thermal energy carried by steam.
The fuel source may include:
-
Oil
-
Gas
-
Coal
-
Firewood
-
Wood chips
-
Rice husks
-
Biomass pellets
-
Sawdust
-
Other types of fuel
When the fuel burns, the heat generated is transferred through the boiler’s heat-transfer surfaces to the water inside.
Once the water absorbs enough heat, it changes from a liquid into steam.
The steam then carries thermal energy to production equipment throughout the plant. This is the basic operating principle of every boiler system, regardless of the fuel or combustion technology used.
 Diagram illustrating the operating principle of an industrial boiler
III. Why Is It Important to Understand How a Boiler Works?
For someone learning about boilers for the first time, a boiler may appear to be simply a piece of equipment that produces steam.
However, boiler operation involves many related concepts, including:
-
Boiler efficiency
-
Fuel consumption
-
Steam quality
-
Dry steam and wet steam
-
Scale formation
-
Heat-transfer surface cleaning
In practice, all of these factors serve the same objective: ensuring that the heat released from the fuel is converted into steam as efficiently, safely, and economically as possible.
IV. Boiler Classification by Fuel Type
There are several ways to classify industrial boilers.
One of the most common and easiest methods is to classify them according to the type of fuel they use.
Based on this approach, boilers can be divided into two main groups:
| Boiler Group | Fuels Used | Main Characteristics |
| Liquid-fuel boilers | Diesel oil, fuel oil, LPG, CNG, and other gaseous fuels | Cleaner operation, a high level of automation, and generally higher fuel costs |
| Solid-fuel boilers | Coal, firewood, wood chips, sawdust, rice husks, biomass pellets, and other solid fuels | Can use a wide range of fuels, but the combustion technology must be selected to match the fuel characteristics |
1. Liquid-Fuel Boilers
The first group consists of liquid-fuel boilers that generate heat through fuel combustion.
Common fuels include:
-
Diesel oil
-
Fuel oil
-
LPG
-
CNG
-
Other gaseous fuels
In this type of boiler, the fuel is supplied to a dedicated burner, mixed with air, and ignited to create a flame that heats the water inside the boiler.
A simple way to understand the operating principle of an oil or gas burner is to compare it with a household gas stove.
However, industrial burners are far more complex because they must meet much higher requirements for capacity, operating stability, and safety.
 Industrial burner system installed on a liquid-fuel or gas-fired boiler
How Does an Industrial Burner Work?
An industrial burner does more than simply feed fuel into the combustion chamber.
To ensure stable and safe combustion, it also integrates a range of control and protection systems, including:
-
Combustion air supply system
-
Ignition system
-
Flame monitoring system
-
Fuel safety valves
-
Pressure sensors
-
Temperature sensors
-
Other safety interlocks
Together, these systems allow the combustion process to be controlled automatically, reduce dependence on the operator, and improve overall operating safety.
Advantages of Liquid-Fuel Boilers
The most notable advantages of this boiler group are clean operation and a high level of automation.
Compared with solid-fuel boilers, Liquid-fuel boiler generally offer the following benefits:
-
Cleaner operation
-
Easier load adjustment
-
Higher automation
-
No ash or slag generated during combustion
These characteristics make boiler operation and load control more convenient in many industrial applications.
Disadvantages of Liquid-Fuel Boilers
Despite their operational advantages, these boilers also have one major limitation: fuel cost.
When DIESEL oil, LPG, or CNG is used, the cost of producing one ton of steam is usually significantly higher than with biomass or coal-fired boilers.
For this reason, businesses should carefully balance the initial investment cost, fuel cost, and actual operating requirements before selecting a suitable boiler technology.
When Should You Choose an Liquid-Fuel Boilers
Liquid-fuel boilers are often suitable for factories that:
-
Require a high level of cleanliness in production
-
Have limited installation space
-
Cannot allow dust, ash, or slag generation
-
Have a relatively small steam demand
-
Do not operate continuously
The decision should be based on the production characteristics and operating requirements of each facility rather than on the initial investment cost alone.
2. Solid-Fuel Boilers
Solid-fuel boilers are widely used across many industries, particularly in factories with high steam demand and a stable supply of biomass or coal.
Common solid fuels include:
-
Coal
-
Firewood
-
Wood logs
-
Sawdust
-
Rice husks
-
Wood pellets
-
Rice husk pellets
-
Tree bark
-
Cashew shell waste
-
Agricultural residues
-
Various other biomass fuels
Why Are Solid-Fuel Boilers Classified by Combustion Technology?
Unlike liquid- or gas-fired boilers, solid-fuel boilers are not classified solely by the type of fuel they burn.
Even when using solid fuels, each fuel has different characteristics in terms of:
-
Particle size
-
Moisture content
-
Heating value
-
Ash content
-
Ignition characteristics
Because of these differences, selecting the appropriate combustion technology is just as important as selecting the fuel itself.
If the wrong combustion technology is used, the boiler may experience problems such as:
-
Failure to achieve the designed steam capacity
-
Excessive fuel consumption
-
Difficulty meeting environmental emission requirements
-
More demanding day-to-day operation
-
Increased risk of operational issues
The most common solid-fuel combustion technologies include:
-
Fixed-grate boilers
-
Chain-grate boilers
-
Fluidized bed boilers
-
Suspension-fired boilers
In this article, we will first examine fixed-grate boilers and chain-grate boilers. The remaining combustion technologies will be covered in detail in the next articles of this series.
What Is a Fixed-Grate Boiler?
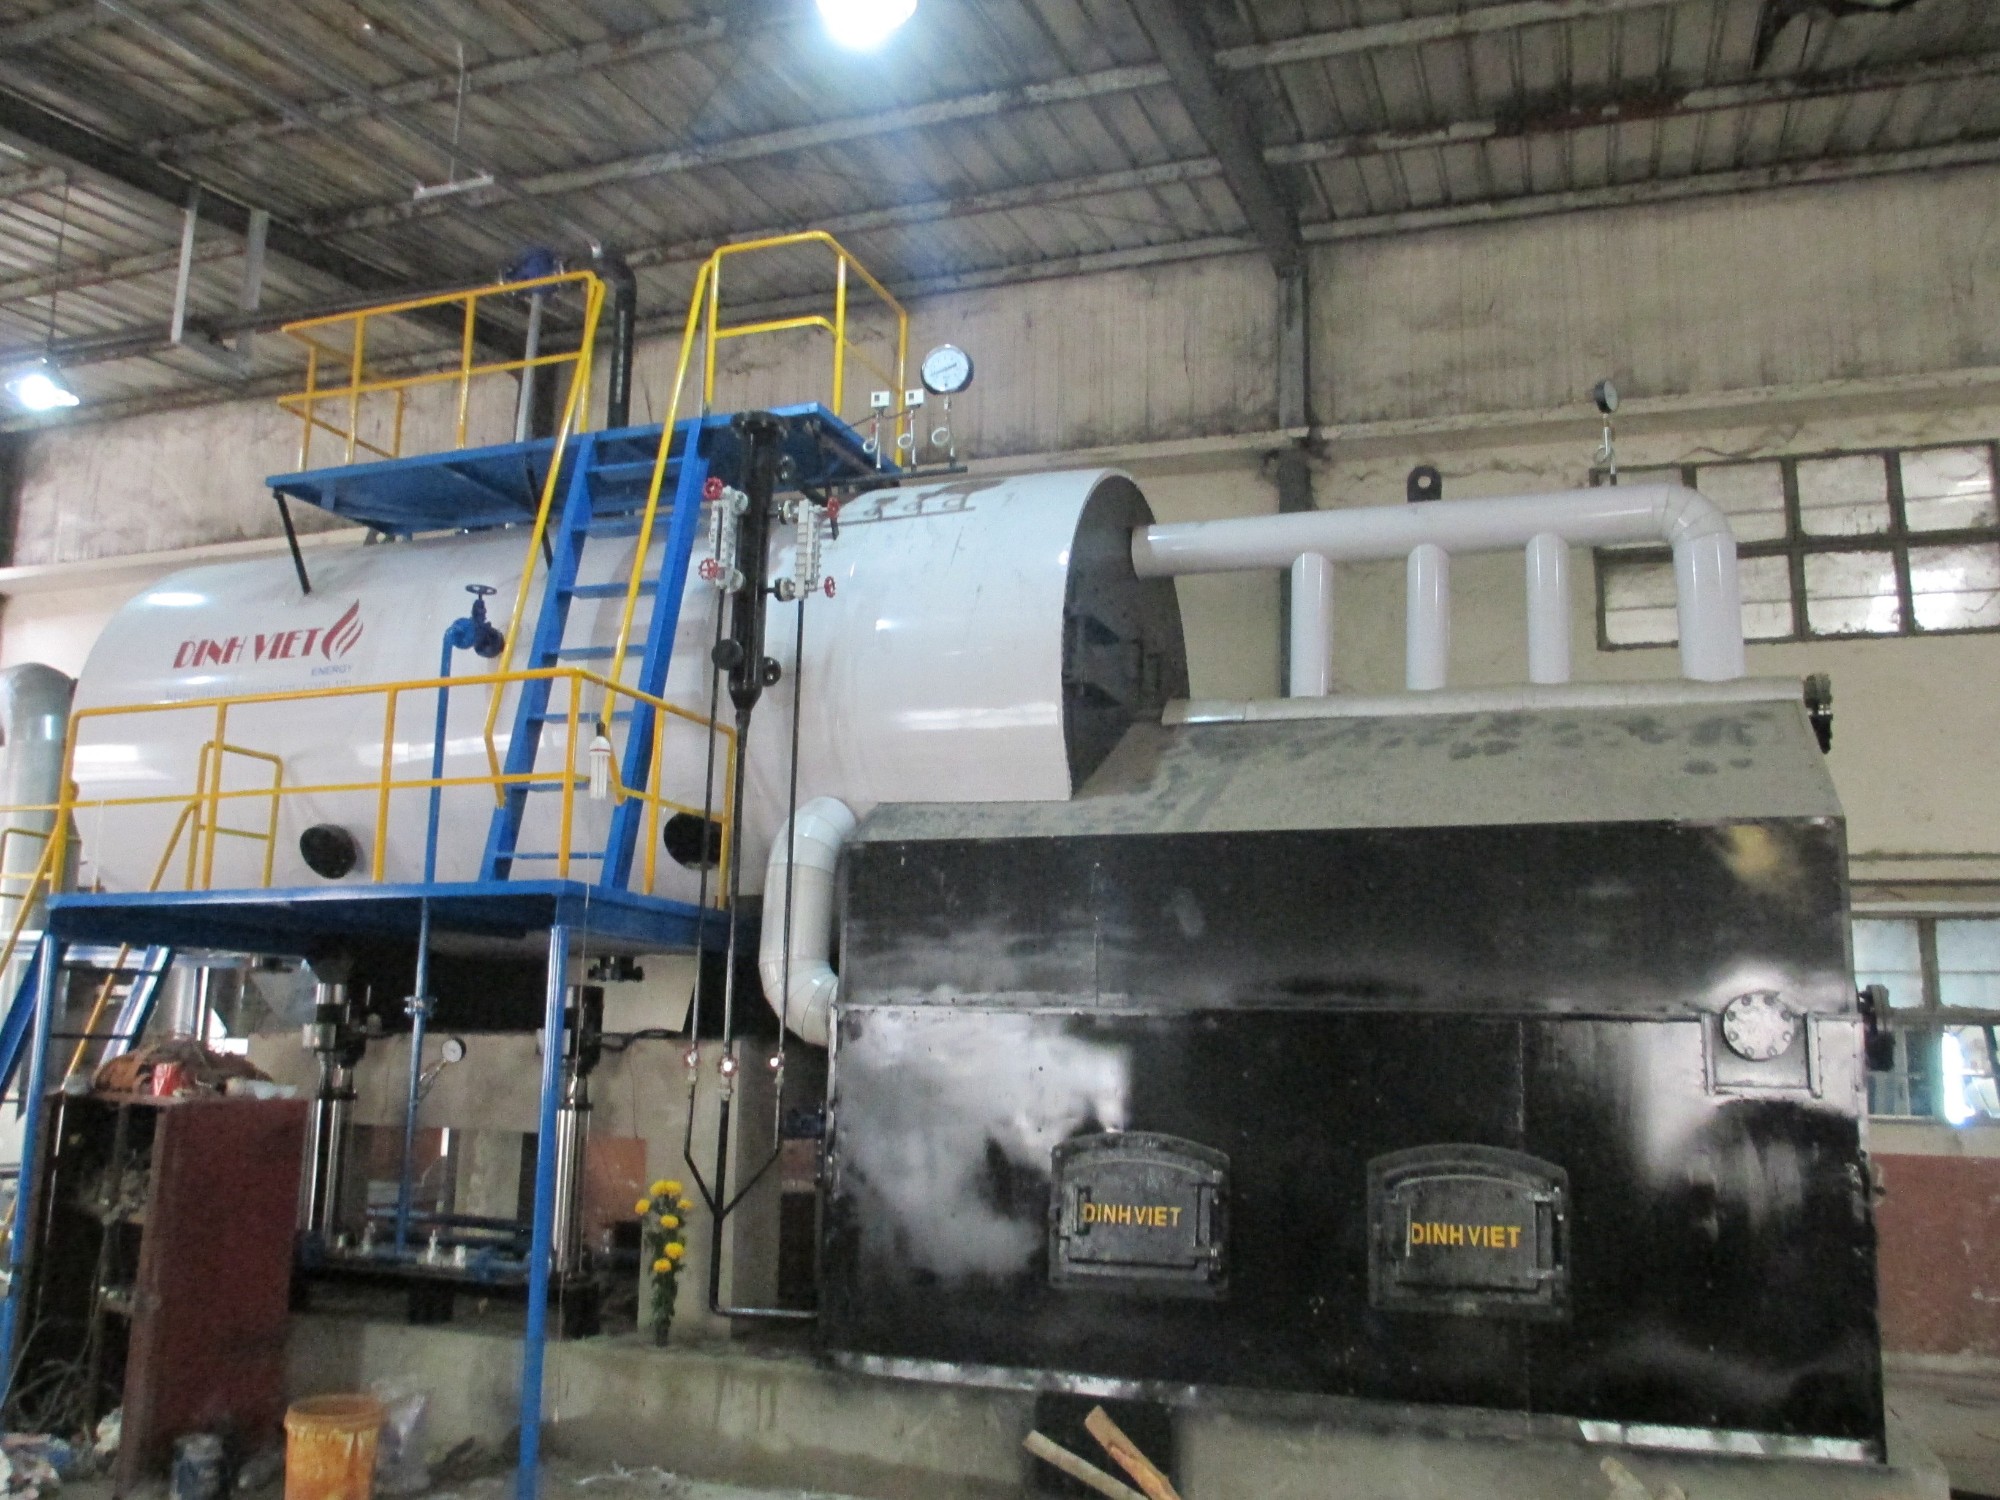
 A fixed-grate boiler burns fuel on a stationary grate to generate steam through heat transfer
A fixed-grate boiler is one of the oldest and most widely recognized solid-fuel combustion technologies. Its relatively simple design has made it a popular choice for many small industrial facilities.
In this type of boiler, fuel is manually or mechanically placed onto a stationary grate inside the furnace.
Combustion air is supplied from beneath the grate, allowing the fuel to burn on its surface. After combustion, ash and slag fall below the grate or are removed manually.
Fuels Suitable for Fixed-Grate Boilers
Fixed-grate boilers are generally suitable for relatively large-sized fuels, including:
-
Lump coal
-
Coke
-
Firewood
-
Chipped wood
-
Compressed sawdust logs
-
Wood briquettes
-
Other large solid fuels
These fuels are well suited to a stationary grate, where they are loaded directly onto the grate surface to sustain combustion.
Operating Characteristics of Fixed-Grate Boilers
One of the defining characteristics of a fixed-grate boiler is that much of the fuel-handling process is still performed manually.
Operators are responsible for feeding fuel into the furnace, monitoring combustion, and removing ash and slag during operation.
As a result, combustion stability depends heavily on the operator's experience and operating practices.
Advantages of Fixed-Grate Boilers
Fixed-grate boilers offer several advantages, including:
-
Relatively simple construction
-
Low initial investment cost
-
Compact design
-
Easy transportation
-
Straightforward installation
-
Simple maintenance
For facilities with relatively low steam demand, large-sized fuel, and limited investment budgets, this technology can still be a practical solution.
Limitations of Fixed-Grate Boilers
Despite their advantages in terms of simple construction and low investment cost, fixed-grate boilers also have several limitations.
The biggest drawback of this technology is its heavy reliance on manual operation.
Factors such as how much fuel is added, how evenly it is distributed, how combustion air is adjusted, and how ash is removed all have a direct impact on the combustion process inside the furnace.
If the operator lacks sufficient experience, combustion can become unstable due to inconsistent fuel feeding or improper air supply. As a result, fuel efficiency decreases, fuel consumption increases, and flue gas emissions become more difficult to control.
When Should You Choose a Fixed-Grate Boiler?
A fixed-grate boiler can still be an appropriate choice under certain operating conditions.
In particular, it is generally suitable for systems with a steam capacity of up to approximately 5 tons per hour, provided that the fuel characteristics and production requirements are compatible with this technology.
However, when the required capacity exceeds approximately 5 tons of steam per hour, maintaining stable combustion with a manually fired fixed grate becomes increasingly difficult.
This is because manual fuel feeding has practical limitations, while the amount of fuel required and the complexity of combustion control increase significantly as boiler capacity grows.
What Is a Chain-Grate Boiler?
Another solid-fuel combustion technology widely used in industry is the chain-grate boiler.
The most significant difference between a chain-grate boiler and a fixed-grate boiler lies in the grate system itself.
While a fixed-grate boiler uses a stationary grate with mostly manual fuel feeding, a chain-grate boiler uses a continuously moving metal grate that operates similarly to a conveyor inside the furnace.
Fuel is fed onto one end of the moving grate. As the grate advances, the fuel passes through the combustion zone, burns progressively along the grate, and the remaining ash is discharged at the opposite end.
Operating Characteristics of Chain-Grate Boilers
Because the grate moves continuously, fuel is distributed more evenly than in a fixed-grate boiler.
This provides several operational advantages:
-
Reduced dependence on manual fuel feeding
-
More stable combustion
-
A higher level of automation
For this reason, chain-grate boilers became a popular choice for facilities requiring greater steam capacity than fixed-grate boilers could efficiently provide.
Fuels Suitable for Chain-Grate Boilers
Chain-grate boilers generally perform best with fuels that have relatively consistent physical properties.
For optimum operation, the fuel should have:
-
Small and uniform particle size
-
Moderate moisture content
-
Relatively high heating value
-
Low impurity content
In most applications, the fuel size should generally be less than approximately 50 mm to ensure smooth fuel feeding and efficient combustion.
Advantages of Chain-Grate Boilers
Compared with fixed-grate boilers, chain-grate boilers offer several operational advantages:
-
Relatively compact design
-
More stable combustion
-
Reduced dependence on operator skill
-
Suitable for a variety of relatively uniform solid fuels
When the fuel has appropriate moisture content, consistent quality, and does not produce excessive slagging, chain-grate boilers can deliver reliable combustion performance and stable operation.
Limitations of Chain-Grate Boilers
Despite their higher level of automation, chain-grate boilers also have certain limitations.
As highlighted in the original content, the most critical component is the moving grate system itself.
This mechanical assembly operates continuously in a high-temperature environment while being exposed to:
-
Ash and slag
-
Mechanical wear
-
Thermal deformation
-
Variations in fuel quality
When fuel has high moisture content, inconsistent particle size, excessive impurities, or a strong tendency to form slag, the moving grate is more likely to experience wear or damage if combustion is not properly controlled.
Repair Costs of a Damaged Chain Grate
Repairing a chain-grate system is often a complex process.
In many cases, a boiler may need to be shut down for 3 to 7 days to repair or replace damaged grate components.
Such downtime affects not only the boiler itself but may also disrupt the plant's production schedule if no backup steam source is available.
Why Are Chain-Grate Boilers Used Less Frequently Today?
In Vietnam, many industrial facilities have experienced the limitations of chain-grate technology, particularly when burning biomass fuels with widely varying moisture content and fuel quality.
This is one of the reasons why chain-grate boilers are used less frequently today than in the past, especially for projects that require:
-
Stable operation
-
Lower fuel consumption
-
Compliance with increasingly stringent environmental standards
Selecting the right boiler technology should never be based on steam capacity alone. It should also take into account the type of fuel, environmental requirements, operating conditions, and the company's long-term investment strategy.
When Should You Choose a Chain-Grate Boiler?
Chain-grate boilers are commonly designed for steam capacities ranging from approximately 4 tons per hour to 30 tons per hour or more.
However, choosing this technology should still be based on several practical considerations, including:
-
The actual fuel available
-
Environmental requirements
-
Operating conditions
-
The owner's long-term investment strategy
There is no single boiler technology that is ideal for every application. The most suitable solution depends on the specific production requirements and operating conditions of each facility.
Fixed-Grate vs. Chain-Grate Boilers
| Criteria | Fixed-Grate Boiler | Chain-Grate Boiler |
| Fuel Feeding Principle | Fuel is placed on a stationary grate, with most feeding performed manually | Fuel is continuously fed onto a moving grate and transported through the combustion zone |
| Level of Automation | Low | Higher |
| Dependence on Operator | High | Lower |
| Suitable Fuels | Lump coal, coke, firewood, wood chips, wood briquettes, and other large solid fuels | Small, relatively uniform fuels with moderate moisture content |
| Key Advantages | Simple construction, low investment cost, easy installation, and straightforward maintenance | More stable combustion, more consistent fuel feeding, and reduced dependence on manual operation |
| Main Limitations | Difficult to maintain stable combustion at higher capacities and heavily dependent on operator experience | The moving grate operates under high temperatures and is subject to wear, resulting in higher maintenance and repair requirements |
| Typical Steam Capacity | Up to approximately 5 tons/hour | Approximately 4–30 tons/hour or higher |
| Best Suited For | Facilities with relatively low steam demand and limited investment budgets | Facilities requiring higher capacity, greater automation, and relatively consistent fuel quality |
From this comparison, it is clear that both fixed-grate and chain-grate boilers have their own areas of application.
A fixed-grate boiler is generally suitable for smaller steam systems with lower investment costs, while a chain-grate boiler offers greater automation but requires more consistent fuel quality and careful consideration of grate maintenance costs.
For this reason, businesses should select a boiler technology based on actual operating conditions rather than steam capacity or initial investment cost alone.
V. Conclusion
A boiler is a piece of equipment that generates steam for industrial production. However, selecting the right boiler system requires a clear understanding of both its operating principle and the characteristics of different boiler technologies.
In this article, we have covered the fundamental concepts of industrial boilers, including:
-
What a boiler is
-
How a boiler converts fuel into steam
-
Boiler classification by fuel type
-
The operating characteristics of fixed-grate and chain-grate boilers
Each technology has its own strengths and limitations. The best choice should not be based solely on steam capacity or initial investment cost. Fuel type, environmental requirements, level of automation, operating conditions, and long-term business objectives should all be considered.
These fundamental concepts also provide a solid foundation for understanding the more advanced boiler technologies that will be introduced in the next articles from DIVI Group.
In the next part of this series, we will explore fluidized bed boilers, including their operating principles, advantages, limitations, and the reasons why this technology has become a preferred solution for many biomass-fired industrial applications.
VI. Frequently Asked Questions (FAQ)
1. What Is a Boiler?
A boiler is a sealed pressure vessel that uses heat generated from fuel combustion to convert water into steam for a wide range of industrial processes.
2. How Are Industrial Boilers Classified?
Industrial boilers can be classified in several ways.
In this article, boilers are classified according to the type of fuel they use, with two main categories:
-
Liquid- and gas-fired boilers
-
Solid-fuel boilers
3. When Is a Fixed-Grate Boiler the Right Choice?
A fixed-grate boiler is generally suitable for facilities with relatively low steam demand, large-sized solid fuels, and limited investment budgets.
4. What Are the Advantages of a Chain-Grate Boiler?
A chain-grate boiler provides more consistent fuel feeding, a higher level of automation, and reduced dependence on manual operation, resulting in more stable combustion under suitable operating conditions.
5. Which Boiler Technology Is Best for Every Factory?
There is no single boiler technology that is suitable for every application.
The right choice depends on several factors, including the type of fuel available, environmental requirements, production capacity, operating conditions, and the company's long-term investment strategy.
Need Help Choosing the Right Boiler for Your Factory?
The engineering team at DIVI Group is ready to help you:
-
Recommend the most suitable boiler technology for your application
-
Compare the advantages and limitations of different boiler solutions
-
Propose the optimal solution based on your fuel type and operating conditions
-
Design, engineer, and supply complete industrial boiler systems
Contact DIVI Group today for professional technical consultation and a boiler solution tailored to your production requirements.
Other news
-
Industrial Boiler Applications: 6 Common Uses and High-Temperature Heating Solutions
19/08/2026, -
Boiler Types by Design: Water-Tube, Fire-Tube, Single-Drum and Two-Drum Boilers
15/08/2026, -
Fluidized Bed Boiler: Design, Working Principle, Advantages and Disadvantages
07/08/2026, -
8 ENERGY LOSS POINTS THAT INCREASE BOILER FUEL CONSUMPTION AND HOW TO FIX THEM
17/07/2026, -
3 Key Factors That Reduce Boiler Fuel Consumption
08/07/2026, -
Proper Boiler Blowdown Procedure | Safe Boiler Blowdown Valve Operation Guide
24/06/2026, -
What Is PCHR? A Boiler Condensate Recovery Solution That Can Reduce Fuel Consumption by Up to 20%
22/06/2026, -
What Is a Steam Separator? Real-World Testing of Steam Moisture Separation Performance
20/06/2026, -
CHAIN GRATE BOILER VS FLUIDIZED BED BOILER: WHICH TECHNOLOGY IS BETTER FOR YOUR FACTORY?
18/06/2026, -
Oil-Fired Steam Boiler For Chemical Tank Heating
15/06/2026,


DIVI GROUP CO., LTD
Office: 588 Pham Van Chieu street, ward 16, Go Vap district, Ho Chi Minh city, Viet Nam
Factory: Khanh Binh 10 street, Khanh Van quarter, Khanh Binh ward, Tan Uyen city, Binh Duong province, Viet Nam
Hotline: +84 942 488 818
Tel: 0274 3800 338
Email: info@divigroup.com.vn
Business license : 0311016524, issue date : 26/07/2011 by Department of Planning and Investment of Ho Chi Minh City
Representatives: Lê Văn Hiếu
Online :
Vistited :