 EN


Oil-Fired Steam Boiler For Chemical Tank Heating
In metal surface treatment plants, the chemical tank heating system plays a critical role in maintaining stable production processes.
However, many chemical heating systems still face common operational challenges such as:
- Unstable chemical temperatures
- Moisture contamination inside the chemical tanks
- Premature equipment deterioration
- Potential operational safety risks
In this article, DIVI Group introduces a diesel-fired steam boiler solution designed for indirect chemical tank heating using steam.
The system was specifically engineered to support chemical heating processes in metal surface treatment facilities while ensuring safety, reliability, and long-term performance.
Table Of Contents
I. Why Do Chemical Tank Heating Systems Involve Significant Risks?
Many chemical tank heating systems are designed primarily to generate heat, with limited consideration for long-term operational stability and safety.
Over time, this can lead to several issues, including:
- Unstable chemical temperatures
- Moisture entering the chemical solution
- Accelerated equipment wear
- Increased operational risks
For chemical processing applications, temperature control is not merely an operational concern—it directly impacts product quality and production consistency.
This is one of the main reasons why many factories prefer indirect steam heating rather than allowing chemicals to come into direct contact with a heat source.
II. Why Did DIVI Choose Indirect Steam Heating?
For this project, DIVI adopted an indirect steam heating method utilizing a shell-and-tube heat exchanger.
This means that the chemicals never come into direct contact with the heat source.
Instead:
- Steam is generated by the boiler.
- The steam flows through a shell-and-tube heat exchanger.
- Thermal energy is transferred indirectly to the chemical tanks.
Theo thiết kế của hệ thống, đây là phương pháp gia nhiệt được sử dụng nhằm phục vụ cho quá trình gia nhiệt hóa chất trong nhà máy xử lý bề mặt kim loại.
According to the system design, this approach was selected specifically for chemical heating applications within a metal surface treatment plant.
Throughout the project, DIVI emphasized one critical principle:
The chemicals must never come into direct contact with the heat source.
This requirement is fundamental to the safe operation of chemical tank heating systems.
III. Real Project: Chemical Tank Heating System Designed by DIVI
The system was designed and manufactured by DIVI to serve two chemical tanks within a metal surface treatment production line.
The primary objective was to provide indirect chemical heating through steam and a shell-and-tube heat exchanger system.
Beyond simply generating heat, the project required:
- Stable temperature control
- Reliable operation
- Safe system management
- Long-term equipment durability
After evaluating the customer's requirements, DIVI selected a diesel-fired steam boiler combined with an indirect steam heating system.
The solution was custom-engineered specifically for chemical tank heating applications in the metal surface treatment industry.
IV. Overview of DIVI's Diesel-Fired Steam Boiler
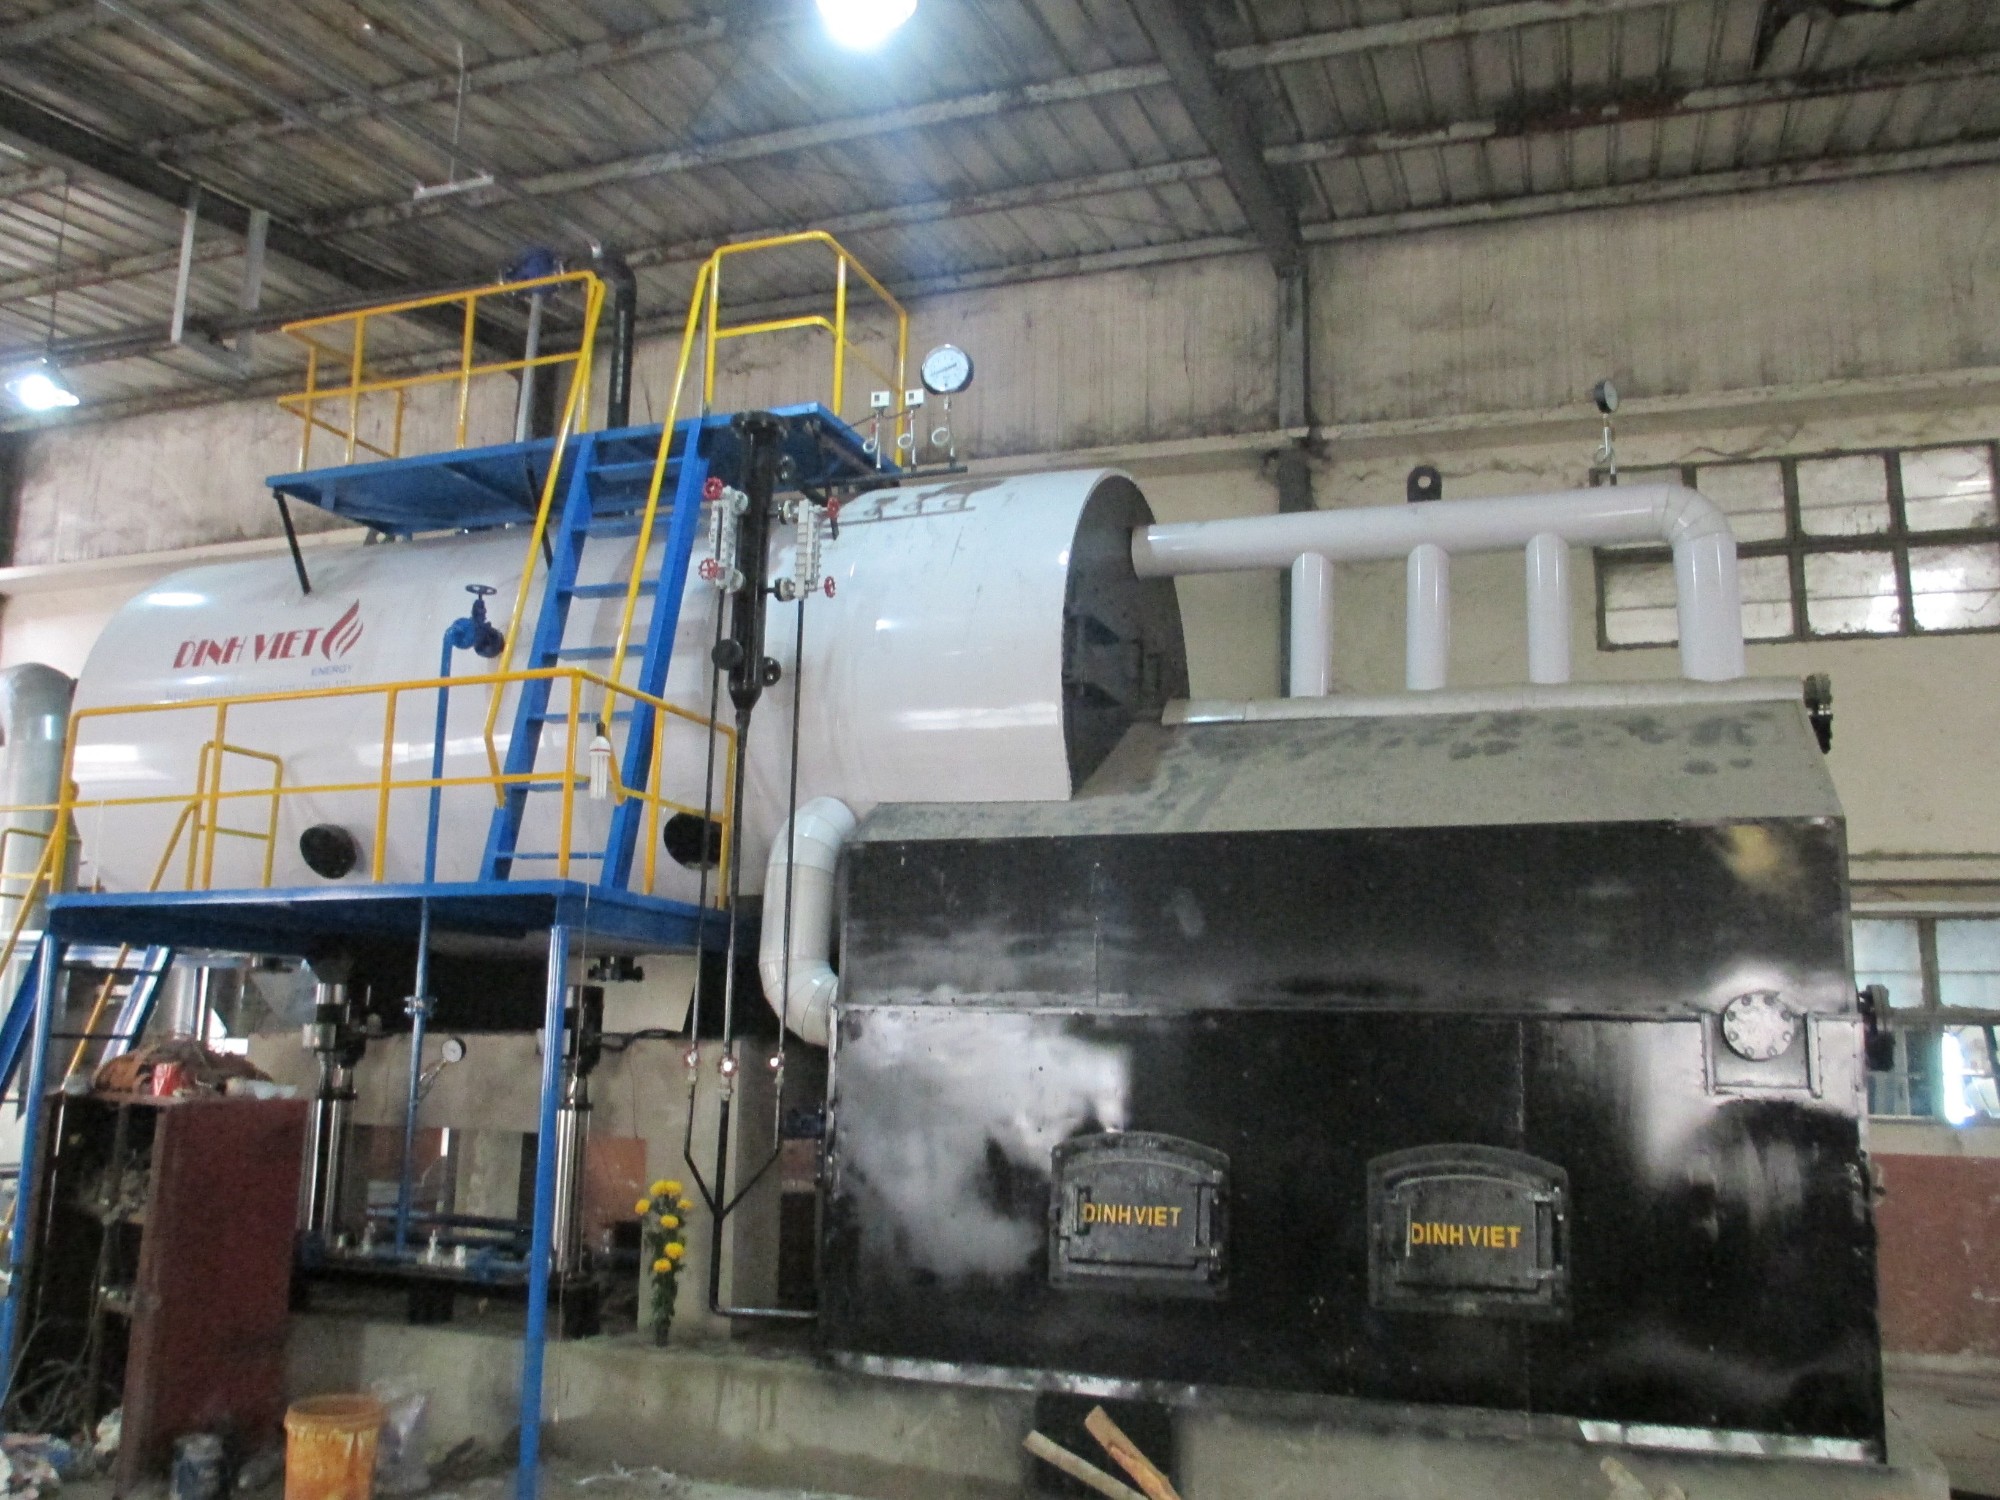
The project utilizes a diesel-fired steam boiler designed and manufactured directly by DIVI.
The boiler features:
- Furnace tube construction
- Fire-tube design
- Three-pass combustion system
- Natural circulation operation
According to the project specifications, this boiler configuration has been widely used for many years and continues to be recognized for its reliability and operational stability.
To facilitate maintenance and inspection, access doors are installed at both the front and rear sections of the boiler.
These access points allow operators to:
- Clean internal surfaces
- Perform equipment inspections
- Replace boiler tubes when necessary
This maintenance-friendly design is one of the notable features of the system.
V. Specialized European Diesel Burner System
The boiler operates using diesel fuel stored in a dedicated fuel tank and supplied to the burner according to the system design.
The project utilizes a specialized European-made diesel burner.
The burner operates using high-pressure atomization technology.
During operation:
- Diesel fuel is atomized into extremely fine droplets.
- The fuel mixes efficiently with combustion air.
- Stable and efficient combustion is achieved.
As the primary heat-generating component, the burner plays a crucial role in the overall performance and reliability of the steam boiler system.
 Specialized diesel burner providing stable and efficient combustion for chemical tank heating applications
VI. Multi-Level Boiler Pressure Protection System
In industrial steam systems, pressure is one of the most critical operating parameters.
To ensure safe and stable operation, DIVI equipped the boiler with five independent pressure protection layers.
This multi-level safety design helps monitor, control, and protect the boiler against abnormal pressure conditions.
1. Dual Safety Valves
Two safety valves are installed directly on the boiler shell.
When the operating pressure exceeds the preset limit, the valves automatically release excess pressure according to their design function.
These safety valves serve as the final mechanical protection layer of the system.
2. Dual Pressure Switches
In addition to the safety valves, the boiler is equipped with two independent pressure switches.
These devices automatically shut down the burner if the pressure exceeds the allowable operating range.
As a result, the system receives an additional level of protection before the safety valves are activated.
3. Pressure Sensor
The system is also equipped with a dedicated pressure sensor.
Its functions include:
- Monitoring real-time operating pressure
- Sending signals to the PLC
- Controlling burner operation
- Supporting automatic pressure regulation
According to the system design, all pressure protection devices operate independently of one another, providing multiple layers of operational safety.
 The boiler is equipped with multiple independent pressure protection devices for safe operation.
VII. Independent Water Level Monitoring System
Pressure is not the only critical parameter in boiler operation.
Water level monitoring is equally important because insufficient water can cause severe damage to the boiler.
For this project, the boiler is equipped with two completely independent water level monitoring systems:
- Float control system
- Electrode probe system
The boiler water level is divided into multiple protection stages, including:
- High water level alarm
- Low water level alarm
- First-stage low-water warning
- Second-stage low-water shutdown protection
If the water level falls to a dangerous condition, the boiler automatically shuts down to prevent equipment damage.
Operators can monitor water levels through:
- Illuminated gauge glass
- FLOWEX LED water level indication system
The monitoring interface is designed to provide clear and intuitive information during daily operation.
 Boiler water levels are monitored through two independent protection systems
VIII. Boiler Feedwater and Water Treatment System
The feedwater system utilizes two FLOWEX feedwater pumps.
According to the project specifications, these pumps are capable of handling temperatures up to 180°C.
Feedwater is supplied from a treated water storage tank.
Before entering the boiler, the water passes through the feedwater treatment system designed specifically for this project.
During the project presentation, DIVI strongly emphasized the importance of feedwater quality.
As highlighted in the project documentation:
"If feedwater is not properly treated, it is no surprise that a boiler deteriorates rapidly after only a few years of operation."
Poor water quality can result in:
- Scale formation
- Corrosion
- Reduced heat transfer efficiency
- Increased fuel consumption
- Shortened equipment lifespan
For this reason, the feedwater treatment system is considered an essential component of the overall solution.
 Feedwater is properly treated before entering the boiler system.
IX. PLC-Based Control System
The entire system is controlled by a PLC-based automation platform.
All operating parameters can be configured, monitored, and adjusted through a centralized touchscreen HMI.
According to the project configuration, the PLC serves as the central control unit for the entire diesel-fired steam boiler and chemical tank heating system.
X. Steam Distribution and Chemical Tank Heating System
Steam generated by the boiler is first routed to a steam header, where pressure is stabilized before being supplied to downstream equipment.
A steam trap station is installed beneath the steam header to automatically discharge condensate from the steam distribution piping, ensuring dry steam is delivered throughout the system.
The steam is then transferred to the chemical tanks through a shell-and-tube heat exchanger, providing safe and efficient indirect heating.
Because the chemicals are completely isolated from the steam, the system eliminates the risk of contamination while maintaining precise temperature control.
A dedicated steam control valve assembly regulates the steam flow rate, allowing operators to maintain the required chemical tank temperature under varying production conditions.
Additional isolation valves are provided to simplify maintenance and improve operational flexibility.
XI. Condensate Recovery System
Following heat transfer, the condensate is collected and returned to the boiler feedwater system to improve overall energy efficiency.
The condensate recovery station utilizes a float-type steam trap and includes:
- Isolation valves
- Strainer
- Sight glass
- Check valve
This configuration ensures reliable condensate removal, reduces heat losses, minimizes boiler fuel consumption, and improves the overall efficiency of the steam system.
By recovering hot condensate and returning it to the boiler, the system significantly reduces operating costs while enhancing long-term boiler performance.
XII. Technical Specifications Overview
| System Item | Details |
| Fuel | Diesel Oil |
| Boiler Design | Furnace Tube – Fire Tube |
| Combustion System | Bypass |
| Circulation Method | Natural Water Circulation |
| Heating Method | Indirect Steam Heating |
| Heat Exchanger | Shell-and-Tube Type |
| Control System | PLC-Based Control System |
| Pressure Protection | 5 Independent Protection Layers |
| Water Level Protection | Float Control and Electrode Probe System |
| Condensate Recovery System | Included |
| Industrial Application | Chemical Tank Heating for Metal Surface Treatment Lines |
XIII. Key Points to Remember About Chemical Tank Heating Systems
- The system utilizes an indirect steam heating method.
- The chemical solution never comes into direct contact with the heat source.
- The steam boiler operates on diesel fuel.
- Heat is transferred through a shell-and-tube heat exchanger.
- Operating pressure is monitored through multiple independent protection layers.
- Boiler water levels are controlled by both a float control system and an electrode probe system.
- Feedwater is properly treated before entering the boiler.
- The entire system is operated and monitored through a PLC-based control system.
XIV. Signs That the System Should Be Inspected
During operation, the system should be inspected whenever any of the following conditions are observed:
- Unstable chemical tank temperatures
- Moisture appearing in the chemical solution
- Abnormal operating pressure conditions
- Boiler low-water or high-water level alarms
- Abnormal signals from safety protection devices
These issues were highlighted during the project introduction and should be closely monitored throughout the operation of the system.
XV. FAQ - Frequently Asked Questions
1. Why is indirect steam heating used?
In this system, the chemical solution does not come into direct contact with the heat source.
Heating is achieved through a shell-and-tube heat exchanger that uses steam as the heating medium, ensuring safe and efficient heat transfer.
2. What fuel does the system use?
The steam boiler installed in this project operates on diesel fuel.
3. How is the boiler pressure protected?
The boiler is equipped with:
- 2 safety valves
- 2 pressure switches
- 1 pressure sensor
These devices operate independently to monitor and protect the boiler against abnormal pressure conditions.
4. How is the boiler water level controlled?
The system utilizes both:
- A float control system
- An electrode probe monitoring system
Water levels are divided into multiple protection stages and are displayed through an illuminated gauge glass and an LED indication system.
5. How is the condensate recovery system configured?
Condensate is recovered through a float-type steam trap.
The condensate recovery station is fully equipped with:
- Isolation valves
- Strainers
- Sight glasses
- Check valves
This configuration ensures reliable condensate recovery and efficient operation of the steam system.
XVI. Conclusion
The diesel-fired steam boiler system presented in this project is more than just a steam-generating unit.
It is a complete engineering solution specifically designed for indirect chemical tank heating using steam.
The system includes:
- A diesel-fired steam boiler
- A shell-and-tube heat exchanger
- A PLC-based control system
- A multi-level pressure protection system
- An independent water level monitoring system
- A condensate recovery system
For metal surface treatment plants, selecting the right heating method and designing an appropriate steam heating system are essential factors in achieving safe, stable, and efficient operation.
If your facility is exploring a steam-based chemical tank heating solution, DIVI is ready to conduct a site assessment and recommend the most suitable system based on your actual operating conditions.
Technical Consultation Hotline: +84 942 488 818
Contact DIVI today to discuss the most suitable steam heating solution for your facility.
Other news
-
Industrial Boiler Applications: 6 Common Uses and High-Temperature Heating Solutions
19/08/2026, -
Boiler Types by Design: Water-Tube, Fire-Tube, Single-Drum and Two-Drum Boilers
15/08/2026, -
Fluidized Bed Boiler: Design, Working Principle, Advantages and Disadvantages
07/08/2026, -
What Is a Boiler? How Boilers Work and the Main Types by Fuel
28/07/2026, -
8 ENERGY LOSS POINTS THAT INCREASE BOILER FUEL CONSUMPTION AND HOW TO FIX THEM
17/07/2026, -
3 Key Factors That Reduce Boiler Fuel Consumption
08/07/2026, -
Proper Boiler Blowdown Procedure | Safe Boiler Blowdown Valve Operation Guide
24/06/2026, -
What Is PCHR? A Boiler Condensate Recovery Solution That Can Reduce Fuel Consumption by Up to 20%
22/06/2026, -
What Is a Steam Separator? Real-World Testing of Steam Moisture Separation Performance
20/06/2026, -
CHAIN GRATE BOILER VS FLUIDIZED BED BOILER: WHICH TECHNOLOGY IS BETTER FOR YOUR FACTORY?
18/06/2026,


DIVI GROUP CO., LTD
Office: 588 Pham Van Chieu street, ward 16, Go Vap district, Ho Chi Minh city, Viet Nam
Factory: Khanh Binh 10 street, Khanh Van quarter, Khanh Binh ward, Tan Uyen city, Binh Duong province, Viet Nam
Hotline: +84 942 488 818
Tel: 0274 3800 338
Email: info@divigroup.com.vn
Business license : 0311016524, issue date : 26/07/2011 by Department of Planning and Investment of Ho Chi Minh City
Representatives: Lê Văn Hiếu
Online :
Vistited :